Hard Shell Case manufacturing process — short answer: judge three things: ingress protection (IP67 = 1 m for 30 min), impact structure (26-drop military testing) and foam fit (EVA/PU/XLPE by payload). Details below, standard by standard.
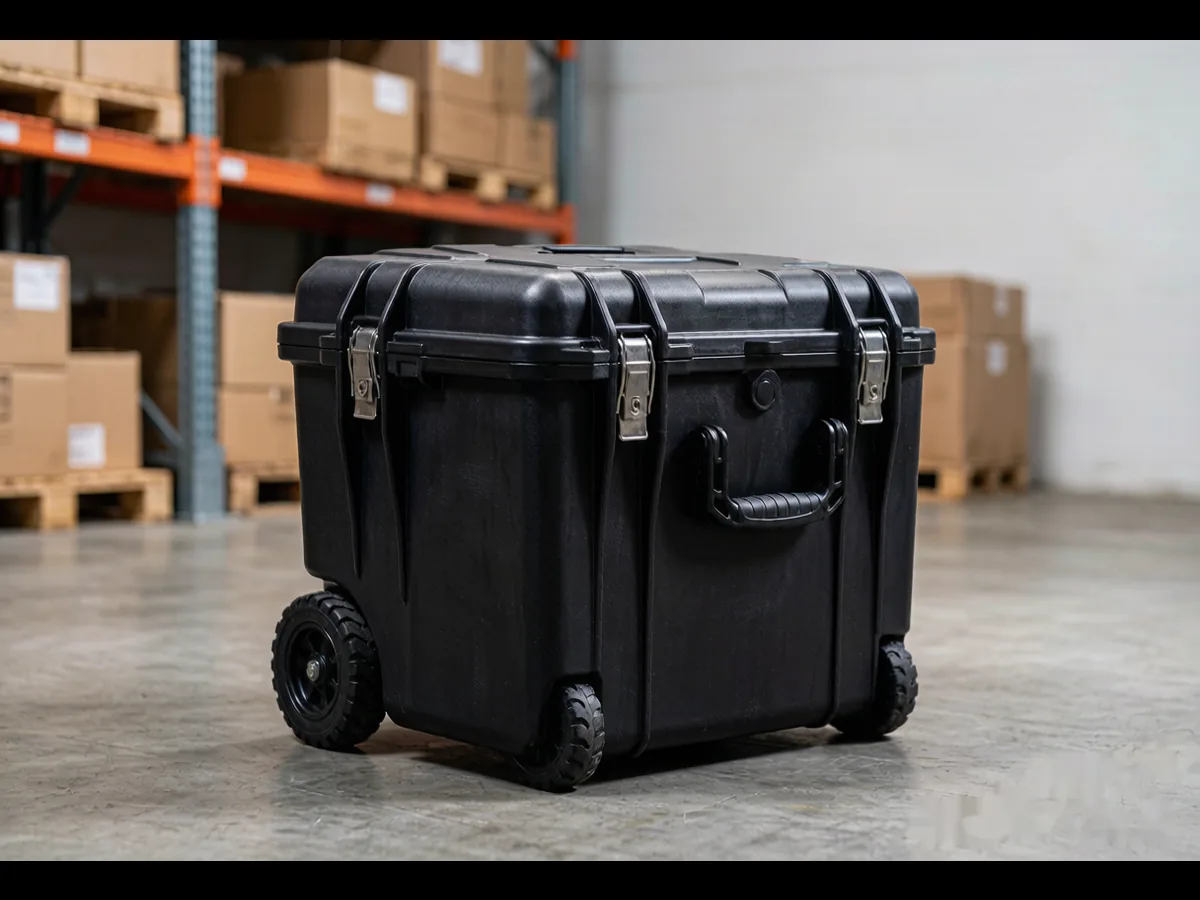
A rotomolded case is produced by rotational molding with seamless walls and high toughness, built for heavy-duty transport of large equipment, spares and hazmat with strong impact and stacking resistance.
Frequently Asked Questions
Tooling cost and timeline?
Can rotomolded cases be insulated or double-walled?
What is the minimum order quantity for custom rotomolded cases?
Rotomolded or injection molded — how do I choose?
Can you run our specified compound?
Will they fade or degrade outdoors?
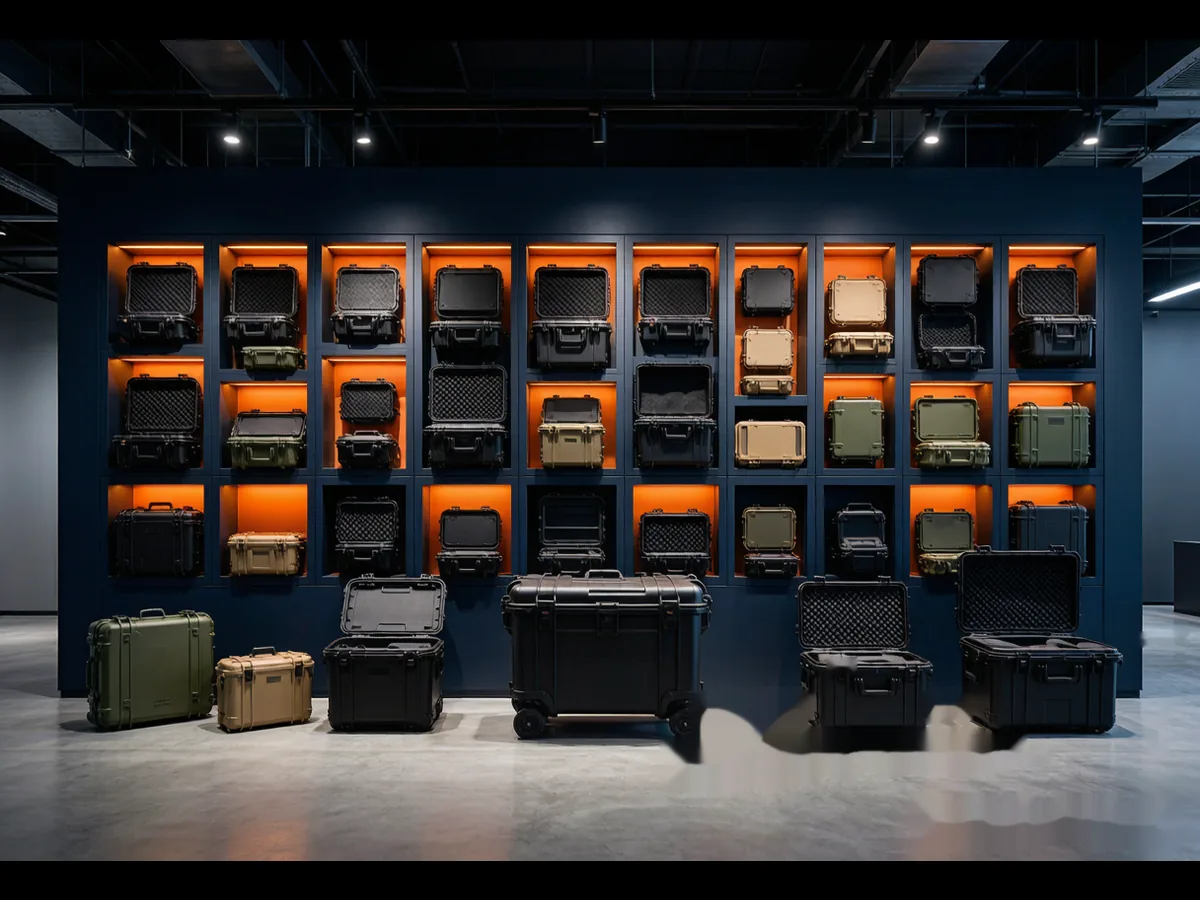
Hard Shell Case manufacturing process: Product & Manufacturer Overview
Rotomolded or injection for your Hard Shell Case manufacturing process? A quick rule: above 800 mm per side or facing brutal handling, choose rotomolding (seamless, tear-resistant); for complex geometry and tight sealing on small-to-mid cases, choose injection. kexinMaterials provides free process selection reviews.
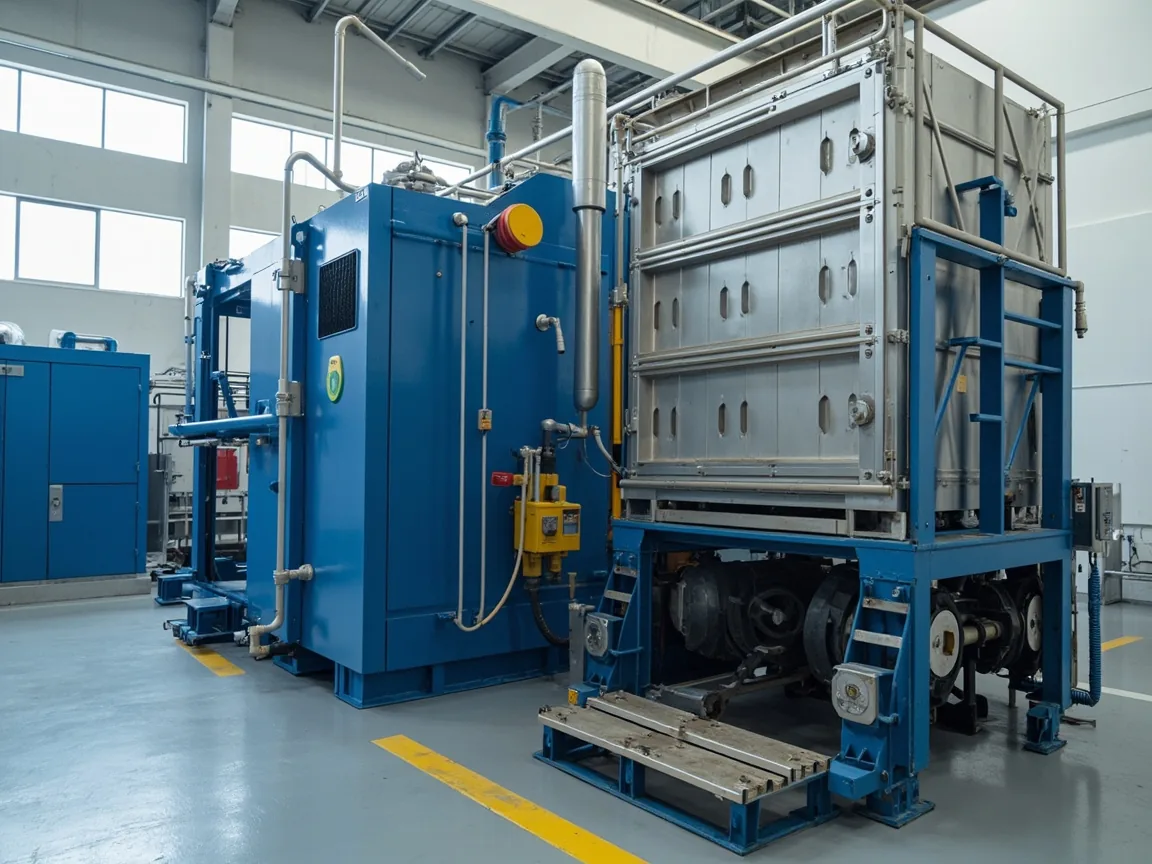
kexinMaterials is a source factory for engineered plastic cases with an in-house tool shop, injection presses up to 2000 tons and rotomolding towers forming 3-meter-class parts — giving OEM/ODM projects deterministic lead times from tooling to mass production.
Key Specifications
| Injection molding | High precision and finish for sealed mid/small cases |
|---|---|
| Rotational molding | Seamless, ultra-tough, for large transit cases |
| Blow molding | Lightweight, low cost, for tool boxes and packaging |
| Materials | Modified PP / ABS / LLDPE / glass-fiber reinforced |
| Tooling | In-house shop, steel and aluminum molds |
| Max part size | 3-meter class via rotomolding |
How kexinMaterials Compares
| Dimension | kexinMaterials | Generic market cases |
|---|---|---|
| Wall uniformity | 5–10 mm seamless rotomold, thicker corners | Injection has weld lines, uneven walls |
| Impact | Monolithic toughness, resists cracking | Thin parts snap |
| Tooling cost | ≈1/5–1/10 of injection, great for large cases | Injection molds costly |
| Size range | Large thick-wall (>1 m) is the sweet spot | Large injection cases pricey |
| MOQ | Friendly for small–mid batches | Economical only at volume |
| Use | Airdrop/transit/marine heavy-load roles | Light-load focus otherwise |
Standards & Industry Data
Military Drop Test (MIL-STD-810H, Method 516.8 Proc. IV)
MIL-STD-810H (8th revision, 2019; 29 test methods) requires transit-drop samples to survive 26 drops from up to 5 ft (1.5 m) onto steel-backed concrete in varied orientations. Versus 810G, the H revision raised drop height from 4 ft to 5 ft and switched to a harder steel-backed surface.
Rotomolding Parameters (LLDPE)
Rotomolded cases use LLDPE powder with typical wall thickness of 5–10 mm (process range 1–16 mm), naturally thicker corners, and no weld seams or trim waste. Tooling costs roughly 1/5–1/10 of injection molds with ~±5% dimensional tolerance — ideal for large, thick-wall cases in small-to-mid batches.
Shell Materials Compared (PP / ABS / PE)
Industry data puts PP (polypropylene) at ~55% of plastic protective-case share — strong chemical resistance, low-temperature toughness and cost efficiency; ABS holds ~30% with harder, glossier surfaces; large thick-wall cases favor rotomolded PE. Plastic/polymer cases together account for 63.7% of the industrial protective case market (2025).
Typical Applications
- Custom rotomolded transit cases for heavy equipment
- High-seal injection molded instrument cases
- Blow-molded tool box contract manufacturing
- Specialty compound case development
- Full ODM outsourcing for case brands
- Export-spec case re-engineering
Buying Questions Answered
For 'Hard Shell Case manufacturing process', the FAQ below gathers what buyers ask most — price structure, MOQ, customization flow and lead time — to speed up your sourcing decision.
When comparing Hard Shell Case manufacturing process suppliers, weigh four things: shell material and wall thickness, seal design and verified ingress rating, interior-foam capability, and whether the factory owns tooling and QC in-house — these decide long-term reliability.
Before sourcing a Hard Shell Case manufacturing process, note the payload's largest dimensions, single-unit weight and shipping mode (air/land/sea). Send those to kexinMaterials and you get a matched case recommendation and quote fastest.
Manufacturing Process
The injection line owns precision and sealing, the rotomolding line owns size and toughness, and the blow molding line owns weight and cost — all sharing one tool shop and QC system, so one supplier covers a multi-process purchasing mix.
Field Case Studies
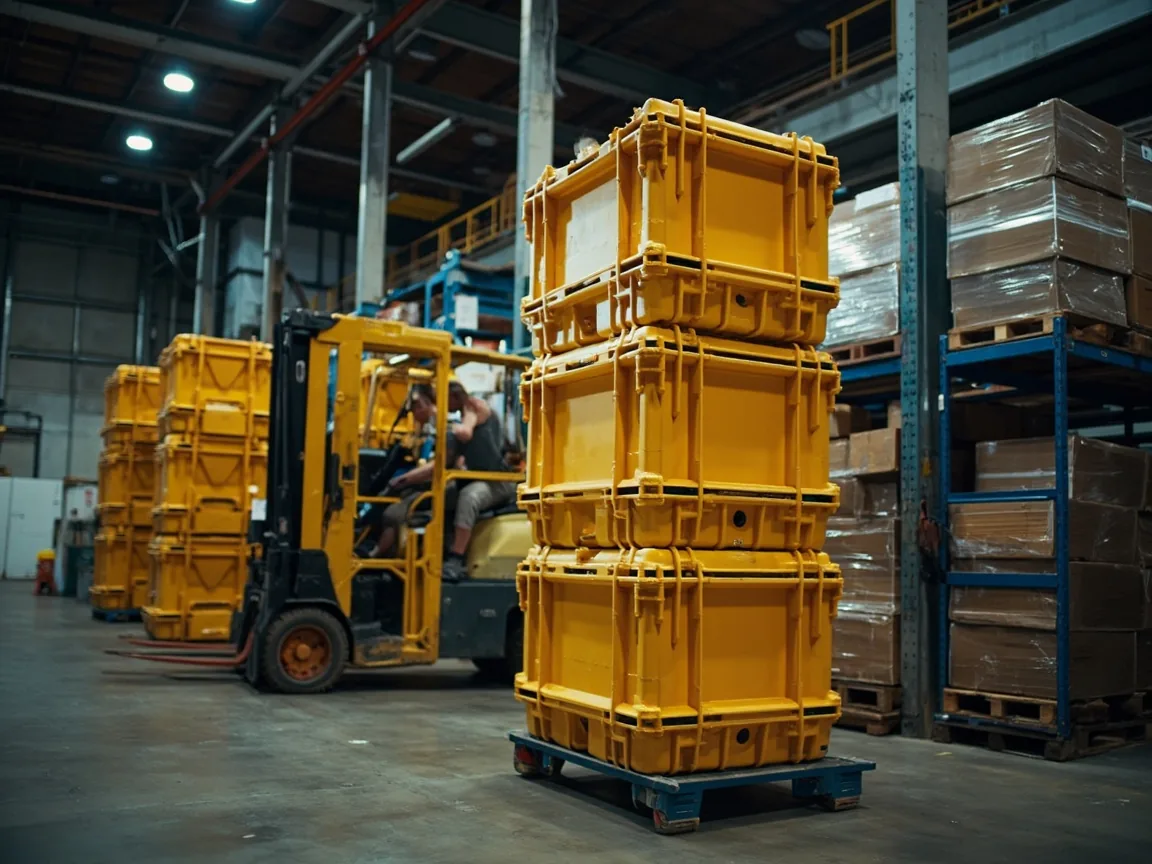
400 large airdrop transit cases, seamless rotomolded 8 mm walls, intact through repeated landing drops.
1,100 thick-wall shipboard cases, salt-fog and impact resistant, no cracking after two years at sea.
About kexinMaterials
KeXin New Materials (Guangdong) Co., Ltd. (brand: kexinMaterials) is a source factory for engineered plastic cases based in Guangdong, China, operating injection, rotational and blow molding lines with an in-house tool shop. Nine product series serve buyers worldwide — from military and drone cases to medical, photography and business lines.
Why kexinMaterials: factory-direct pricing with no middle-man margin; three molding processes under one roof; in-house tooling for controlled lead times; batch drop and seal testing; factory audits, samples-first and third-party QC all supported.